The Future of High-Flow Nozzles: Internal Geometry Matters More Than Length
Five different internal nozzle geometries, measured extrusion force and real flow testing show where the next generation of high-flow hotends may be heading.
One of the most important limits of high-speed FDM/FFF printing is no longer necessarily motion performance, but how quickly the hotend can melt filament uniformly and push it through the nozzle. The experiment shown here approaches that problem not simply by making the melt zone longer, but by comparing several different internal nozzle geometries.
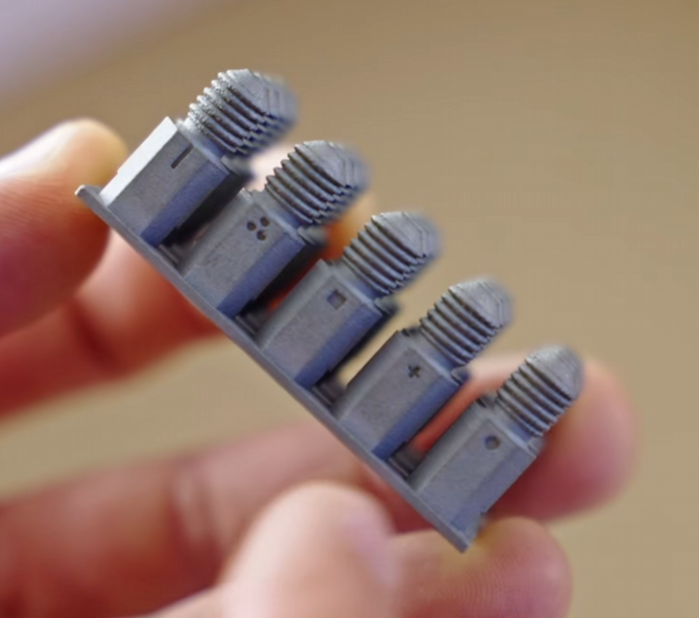
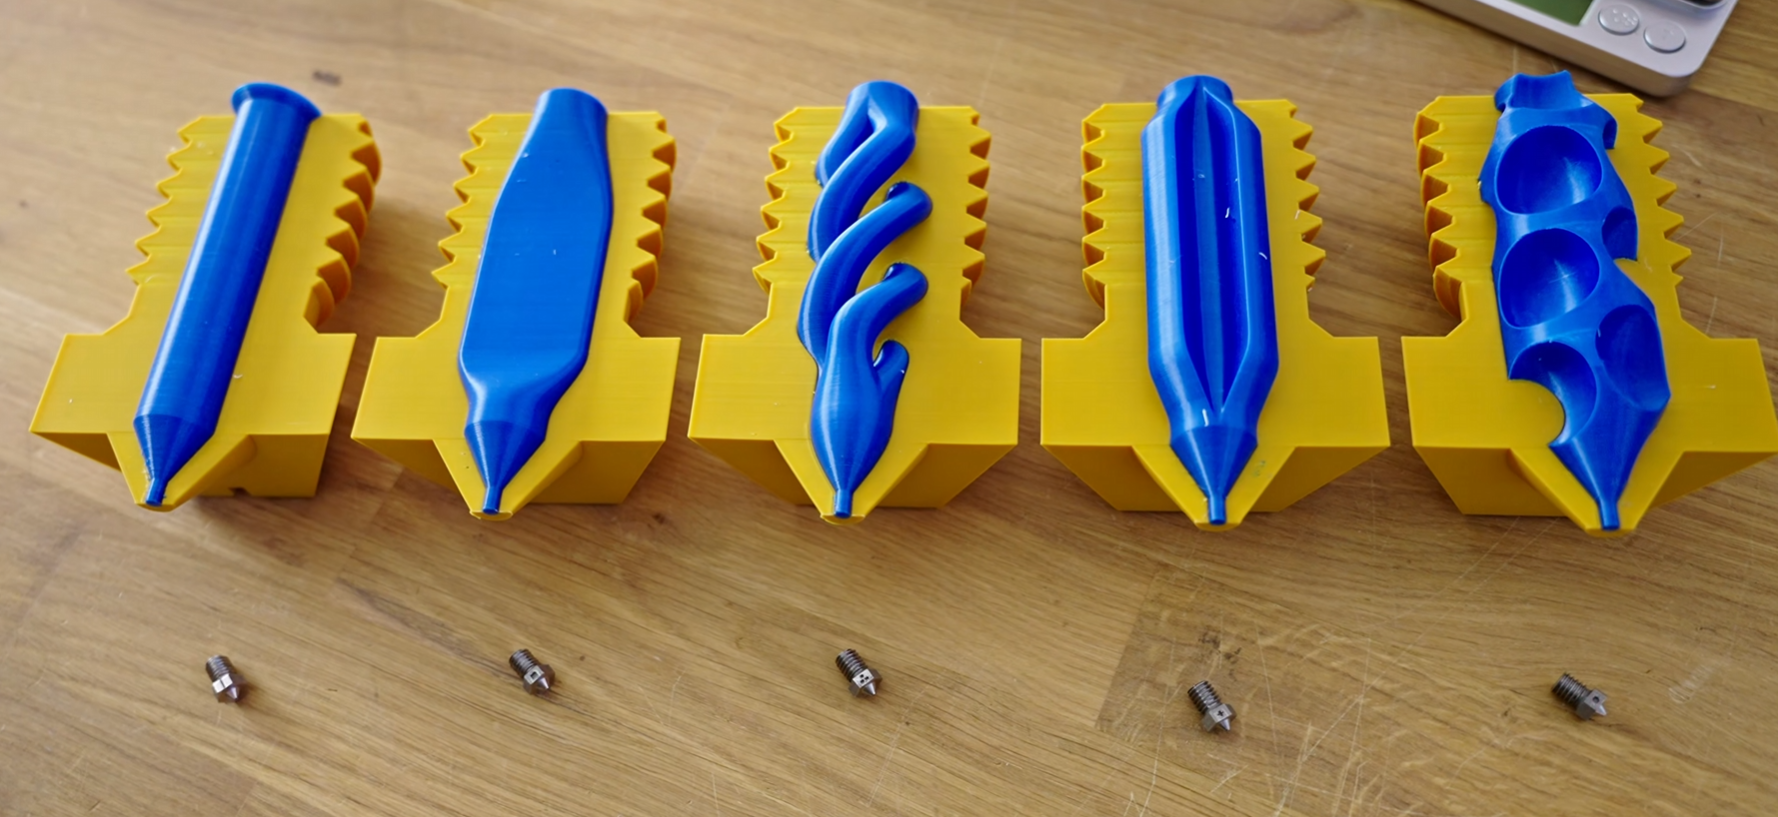
Five different internal designs
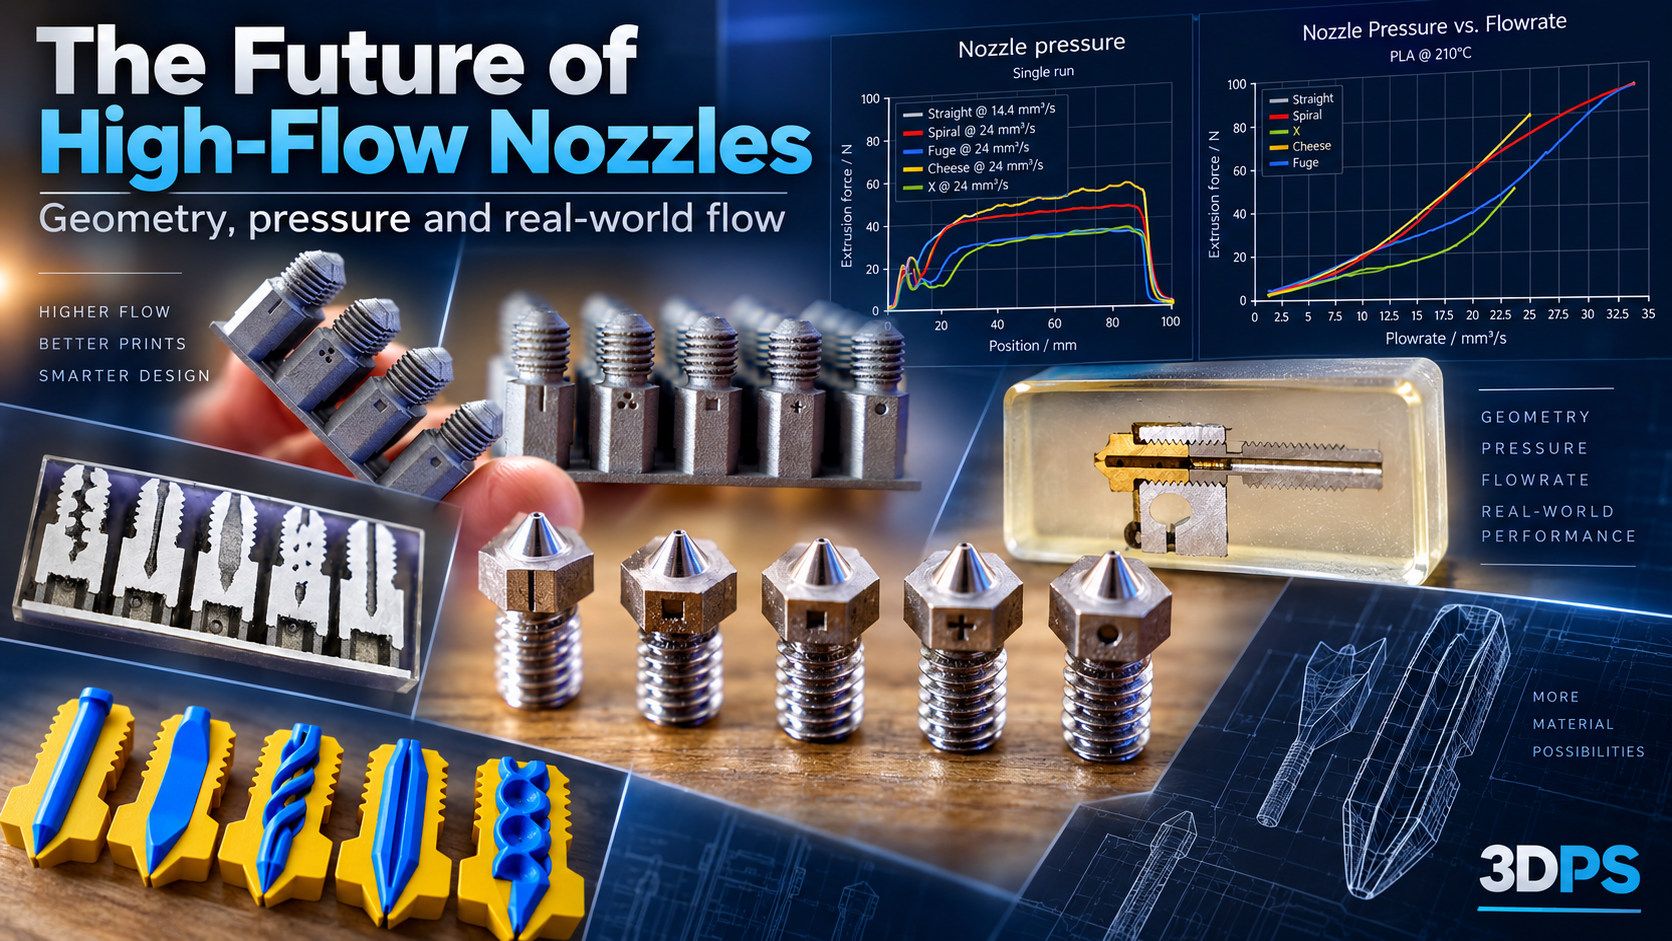
The test compares five designs: Straight, Spiral, X, Cheese and Fuge. From the outside, the nozzles look very similar. The important differences are inside, where the filament path is split, flattened or redirected in different ways to expose more polymer to heated metal surfaces.
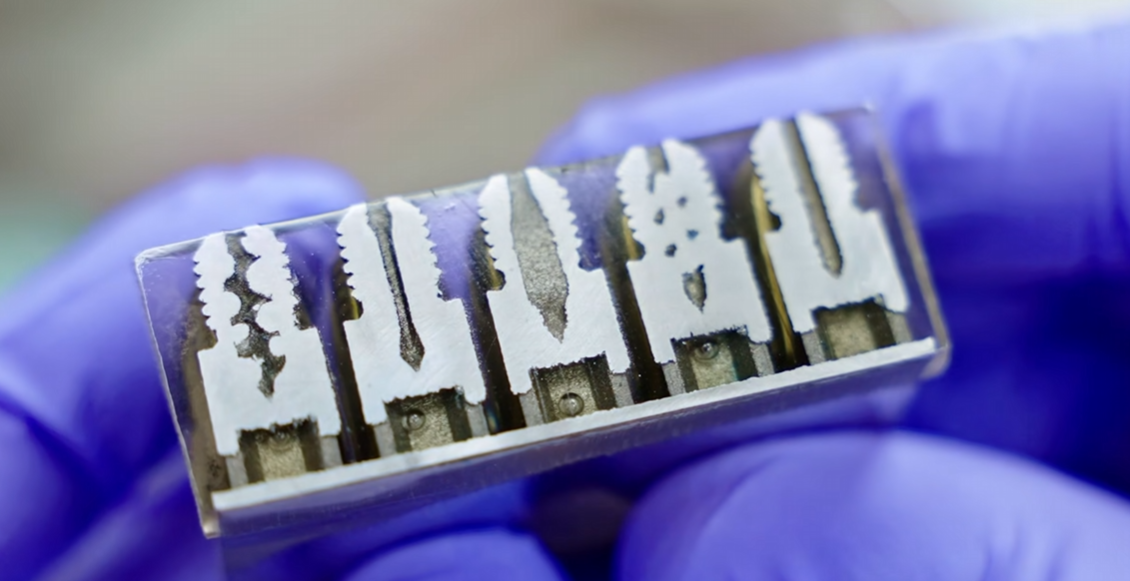
A conventional design uses an almost straight melt path. The experimental geometries instead try to increase heat-transfer area without making the entire hotend substantially longer. That is particularly attractive for modern high-acceleration CoreXY machines, where a compact and lightweight toolhead remains valuable.
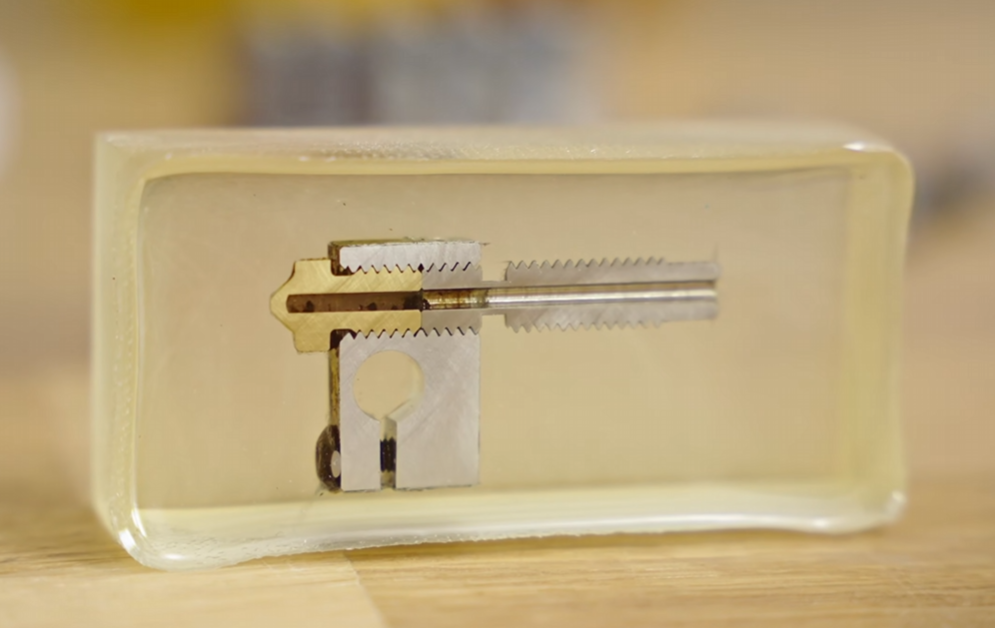
Maximum flow alone is not enough
One of the most important lessons from the test is that maximum volumetric flow does not tell the entire story. If a nozzle can only sustain a certain flow rate by requiring much greater extrusion force, the extruder, filament and printing process are all subjected to higher mechanical load.
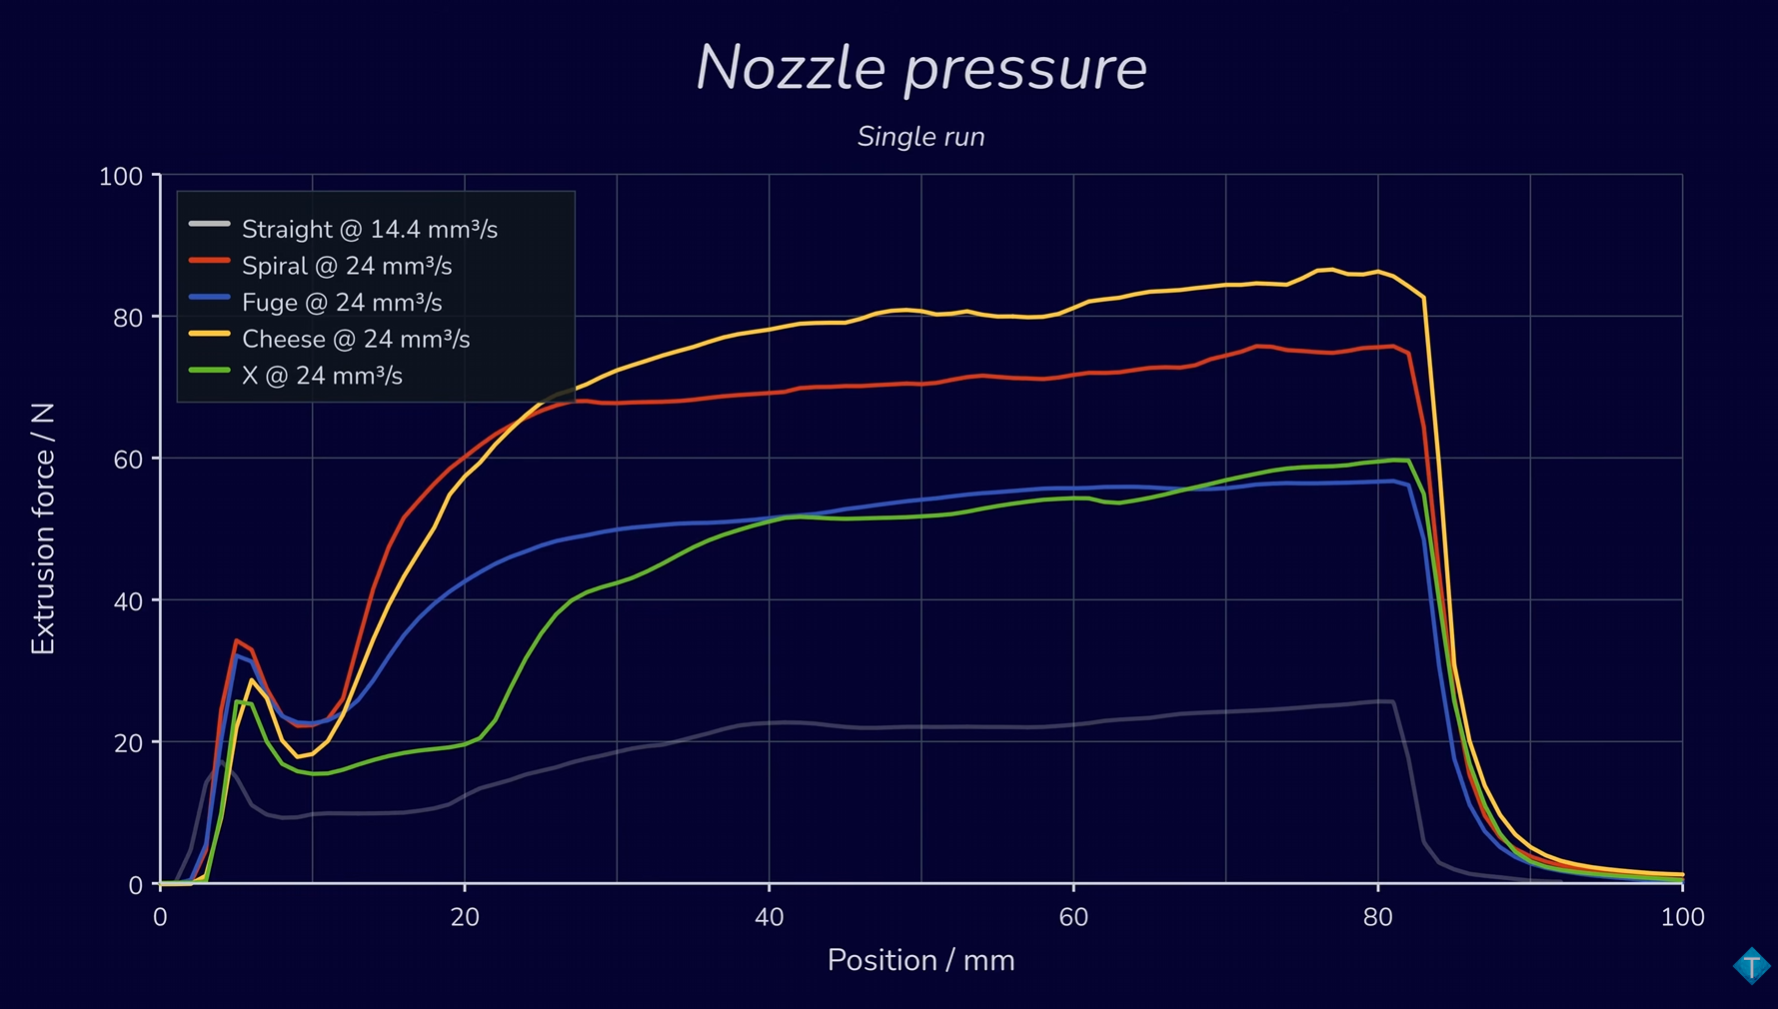
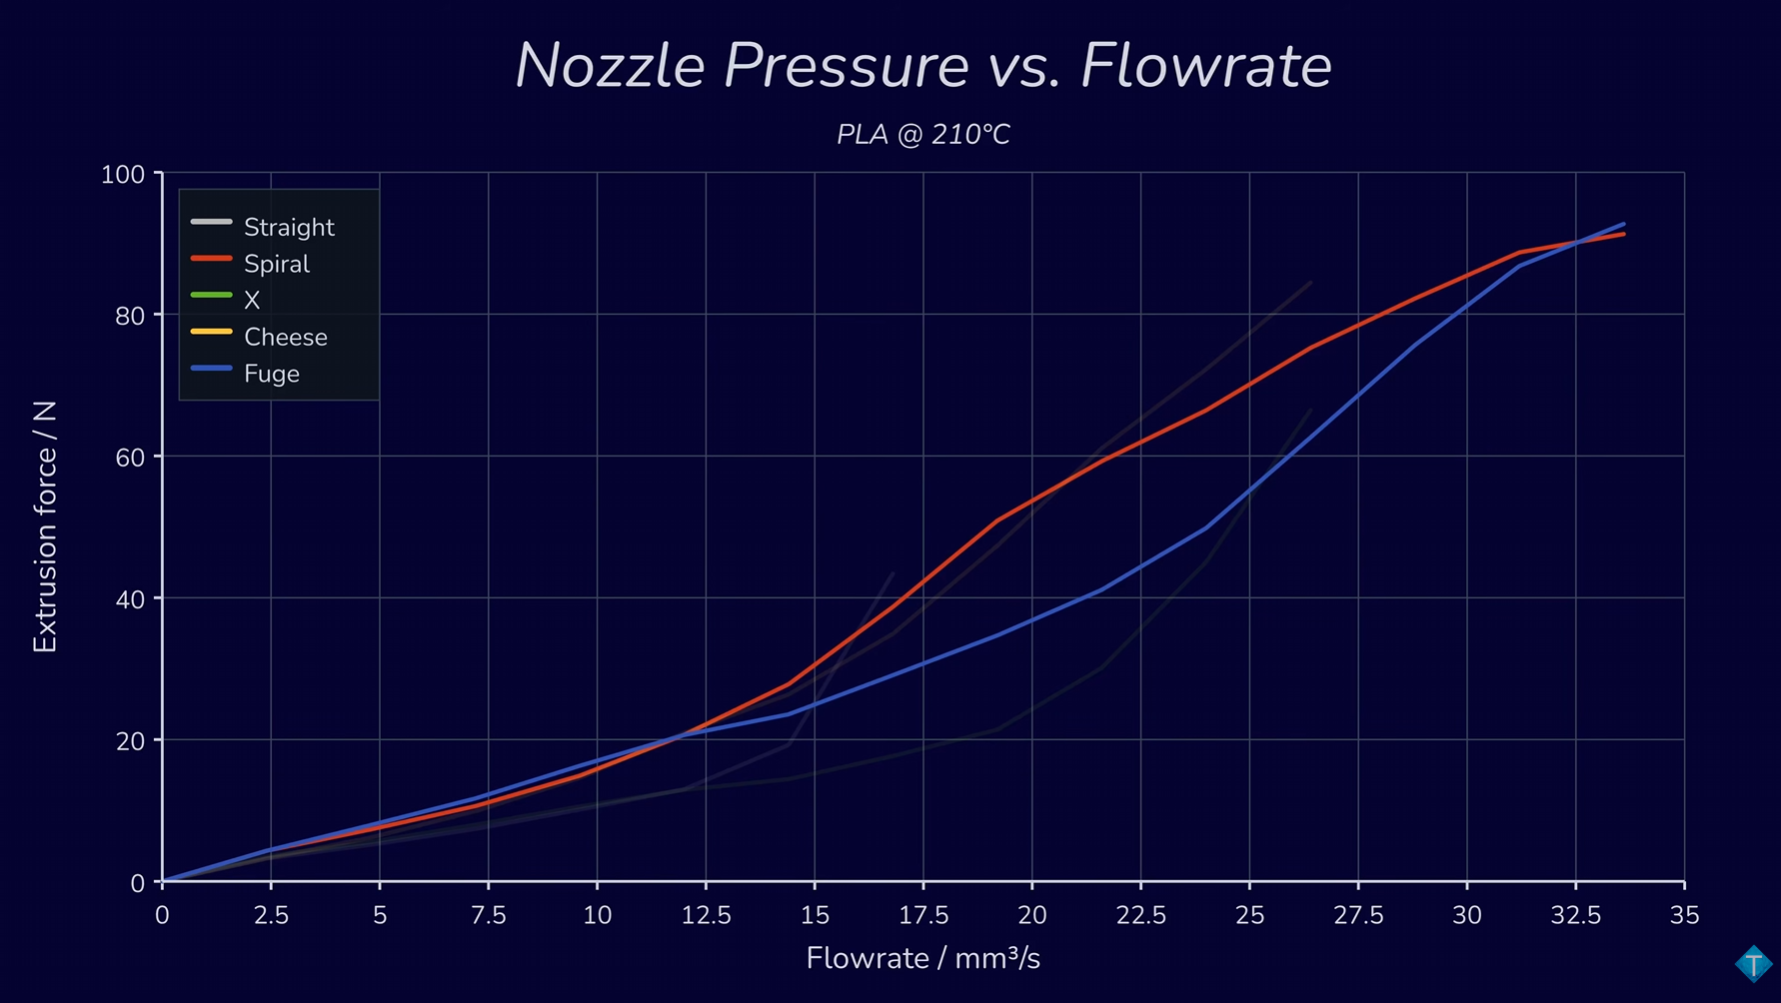
The experiment therefore also measures extrusion force. In one graph, the Straight geometry runs at approximately 14.4 mm³/s, while the Spiral, Fuge, Cheese and X designs are tested at 24 mm³/s. The resulting curves differ considerably, showing that different internal geometry can produce dramatically different nozzle pressure even at the same volumetric flow.
Pressure versus flow is where it gets interesting
The flow-rate test performed with PLA at 210 °C shows that extrusion force does not rise in the same way for every geometry. On the graph, the X design maintains particularly low pressure through a large part of the tested range, while Fuge also shows a favorable curve compared with several more conventional layouts.
Spiral and Cheese can also reach high flow rates, but at higher extrusion force. This is a useful reminder that “high flow” is not a single number. Useful performance depends on material temperature, volumetric flow, extrusion force, stability and ultimately print quality.
Geometry may be the next major step
Traditional high-flow hotends often increase melt-zone length in order to transfer more energy into the polymer. That works, but it also increases physical length and mass, and can make retraction and thermal-management problems harder to control.
The approach shown here points in another direction: melt the material more effectively over the same short distance. Instead of simply extending the hotend, the filament shape and flow path are manipulated inside the nozzle.
What does this mean in practice?
- higher volumetric flow may be possible with a short hotend;
- the extrusion force required for a given flow can potentially be reduced;
- mechanical load on the extruder and filament can be lower;
- heat transfer can improve without making the hotend substantially larger;
- internal geometry may become just as important as nozzle material or nozzle diameter.
The experiment also suggests there may not be one perfect geometry for every application. Different designs behave differently in terms of pressure, flow and likely heat-transfer performance. For next-generation high-flow systems, application- and material-specific internal geometry may therefore become increasingly important.
Source
Video and experiment used as the basis of this article:
YouTube – The future of high-flow nozzles
The measurement images used in this article were provided by the user as frames from the referenced video. The cover image is a 3DPS illustration created from those supplied images.